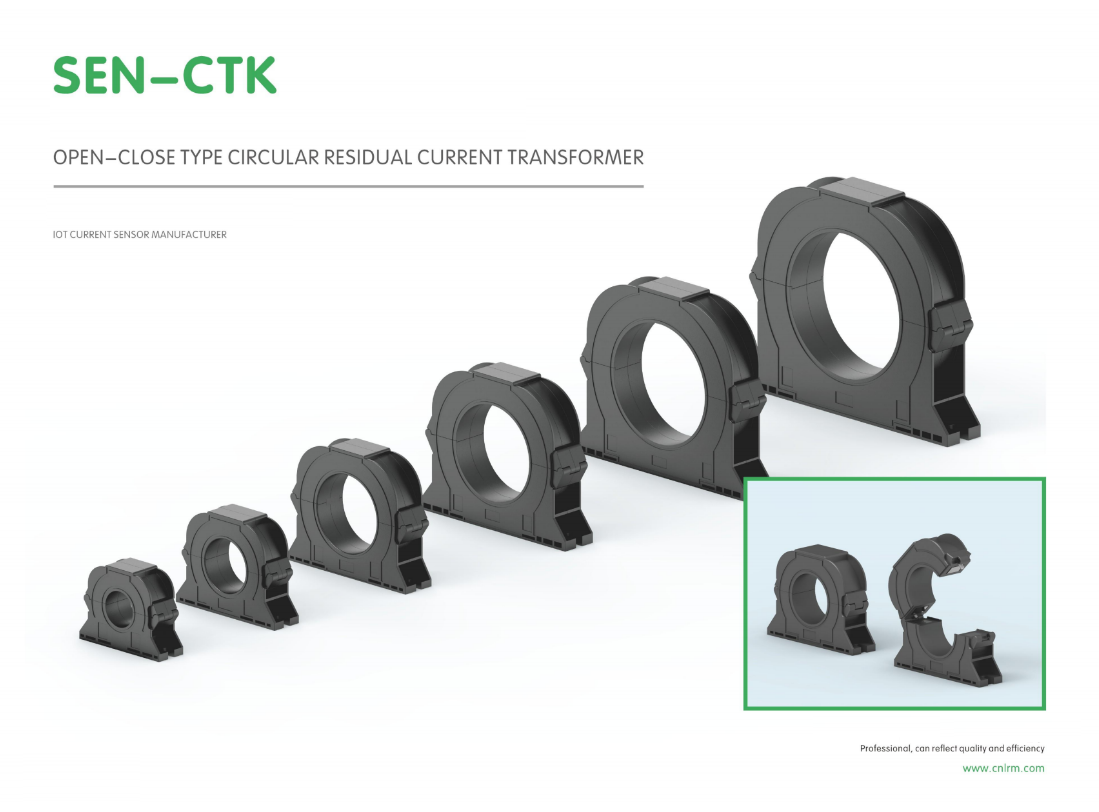
Split-Core Residual Current Transformer Factory Essential Guide to Quality Manufacturing
2026-09-08
What separates a split-core residual current transformer that fails silently from one that protects for decades? The answer usually hides on the factory floor—core material choices, winding tension, insulation testing. This essential guide cuts through spec-sheet noise to spotlight the quality manufacturing steps most buyers never see. Follow along, and you'll also see how Xiasen builds those principles into every unit, helping you source with confidence instead of guesswork.
Core Material Choices That Keep Residual Current Readings Honest
The accuracy of any residual current monitor starts with how the core behaves under tiny differential currents. Standard ferrite cores often drift or saturate when exposed to DC offsets or fluctuating temperatures, which either suppresses the true leakage signal or injects false readings. High-permeability nanocrystalline cores avoid this because their coercivity is exceptionally low and their remanence almost disappears after each half-cycle. That lets the sensor track milliampere-level residual currents without the magnetic history of the core coloring the result.
Mechanical stress and uneven lamination can defeat even a good material choice. When a toroidal core is wound too tightly or the tape layers aren't relaxed through proper annealing, localized saturation points appear and distort the zero-sequence flux. Using a stress-relieved nanocrystalline or permalloy tape wound core keeps domain walls moving uniformly, so the output stays proportional to the actual fault current rather than to incidental asymmetries in the core itself.
Long-term drift is another factor that separates honest readings from misleading ones. Some core materials age poorly, losing permeability or developing oxidation at cut edges that shifts the calibration curve over time. Choosing a core with stable thermal characteristics and sealed edges means the residual current transformer won't quietly wander off its original accuracy class. That way the numbers seen during routine testing still reflect what's happening in the circuit, not the slow degradation of the sensing element.
Winding Tension Control for Stable Leakage Detection
Tension drift during winding rarely announces itself until leak tests start producing scattered results. Even small fluctuations in web or wire tension change the layering density, creating microscopic gaps or crushed edges that behave like intermittent leak paths. Under vacuum or pressure decay testing, these defects produce erratic readings—sometimes passing, sometimes failing—because the sealing surface never settles into a repeatable state. Stable leak detection therefore begins long before the test chamber: it starts with how uniformly the material is wound onto the core.
A closed-loop tension controller that adjusts in real time to roll diameter and line speed does more than prevent breaks. It keeps the interlayer pressure within a narrow band, which directly reduces void formation and mechanical stress at the winding edges. Many operators find that a slight taper tension profile—higher at the core, gradually easing toward the outer layers—improves consistency without sacrificing firmness. Once the winding tension is locked into that repeatable window, leak test results stop jumping around and begin reflecting actual material or seal quality instead of winding artifacts.
Split-Core Assembly Techniques That Minimize Magnetic Loss
Achieving low magnetic loss in split-core designs starts with how the mating surfaces are prepared and aligned. Even microscopic gaps at the interface can force flux to jump across air, raising reluctance and generating localized eddy currents. A common practice is to lap the pole faces to a mirror finish, then apply a thin, uniform layer of high-permeability adhesive or ferrofluid before clamping. This fills any residual roughness and keeps the effective gap below a few micrometers. Additionally, interleaving thin silicon steel laminations across the split line—rather than simply butting two solid halves together—distributes the flux transition over a larger area, reducing fringing and associated loss.
Clamping pressure and alignment also play a decisive role. Too little force leaves micro-gaps; too much can deform the core or stress the magnetic material, increasing hysteresis. Precision dowel pins or self-aligning V-grooves ensure that the two halves register within a few microns every time they are assembled. In field-serviceable designs, a calibrated torque sequence on the clamping bolts helps maintain consistent contact pressure without over-compressing the core. Some manufacturers embed a thin, compressible magnetic shim between the halves, which conforms to surface irregularities while still providing a low-reluctance path.
For high-frequency applications, split cores made from amorphous or nanocrystalline ribbon benefit from a stepped or scarfed joint, where the laminations are cut at an angle and overlapped. This technique extends the effective magnetic path length across the gap and reduces the concentration of flux at any single point. Winding the ribbon continuously and then cutting a single gap with a diamond saw can also minimize burrs and maintain ribbon insulation, further lowering eddy-current losses. Ultimately, the best assembly technique depends on operating frequency, flux density, and whether the core must be repeatedly opened, but all effective methods share a focus on precise gap control, mechanical stability, and material continuity at the split.
Encapsulation Methods That Outlast Harsh Environments
Encapsulation choices for harsh environments rarely come down to a single “best” material. Epoxy potting compounds deliver high mechanical strength and chemical resistance, but their rigidity can transmit stress to solder joints during thermal cycling. Polyurethane, by contrast, stays slightly pliable and cushions components against vibration and repeated expansion-contraction, though it absorbs moisture more readily than epoxy. Silicone gels and elastomers handle extreme cold without cracking, yet their bond strength to substrates is often lower. The trick is matching the failure mode you are actually fighting: thermal shock, salt spray, constant humidity, or a mix of all three.
For thinner protection without adding bulk, conformal coatings such as parylene or acrylate works but parylene's vapor-deposition process creates a truly conformal, pinhole-free layer that resists moisture and solvents far better than brush-on acrylics. However, when the environment demands a hermetic seal, glass-to-metal or ceramic-to-metal encapsulation remains the gold standard for aerospace and downhole sensors. These rigid seals can fail if the coefficient of thermal expansion between the housing and the seal is ignored, so successful designs often pair a flexible inner buffer with a hard outer barrier rather than relying on a single encapsulant to do everything.
Long-term survival depends less on the material datasheet and more on how the encapsulated assembly is validated. Thermal shock cycling, pressurized salt fog, and highly accelerated stress testing reveal weaknesses that static soak tests miss. A common field failure is not the encapsulant degrading outright but losing adhesion at the interface, which creates a microscopic path for moisture to reach the electronics. Because of this, surface preparation and primer selection often matter as much as the encapsulation chemistry itself, especially on low-surface-energy substrates like PTFE or silicone.
Calibration Curves Tuned to Actual Fault Conditions
Protection engineers often start with textbook fault curves, but real-world installations rarely match those idealized assumptions. The presence of arc resistance, non-homogeneous soil, or mutual coupling between parallel feeders can shift the apparent impedance well away from the calculated value. Rather than forcing a generic curve onto the relay, it makes more practical sense to shape the calibration data around what the power system actually does during a fault. This means capturing high-resolution event records from staged tests or naturally occurring disturbances, then using those waveforms to verify that the relay's operating boundary sits comfortably inside the zone of protection without spilling over into load encroachment.
One effective approach is to build a set of fault cases that mirror the specific topology and grounding arrangement of the substation. For instance, a phase-to-phase fault on a short cable feeder may produce a much smaller reactive component than the line impedance suggests, simply because the fault arc behaves like a resistive shunt. By adjusting the calibration points to reflect these measured values, the resulting curve no longer looks like a neat circle or quadrilateral from a manual. Instead, it takes on subtle asymmetries—a wider reach on the resistive axis where arcing is common, a tighter angle on the reactive axis to avoid overreach into the next zone. Technicians who perform secondary injection testing can then verify that the relay trips within the expected time for these non-standard impedance points.
Field experience also shows that seasonal changes in soil moisture or the switching of nearby capacitor banks can nudge the fault loop slightly. A calibration curve that only fits winter conditions may lose security during a summer heatwave when conductor sag increases phase-to-ground faults. Therefore, the tuning process benefits from periodic re-validation: pulling recent fault records, comparing the relay's calculated impedance against a network model, and making small adjustments without overhauling the entire setting group. This keeps the protection responsive to genuine faults while avoiding nuisance trips that erode operator confidence.
End-of-Line Testing Designed to Catch Marginal Units
Many production lines run a basic go/no-go check, but that approach lets units with borderline characteristics slip through. End-of-line testing designed to catch marginal units goes further by exercising each device across its full operating range—voltage, temperature, load, and timing—while looking for small deviations that might not cause immediate failure. The goal isn't just to confirm the unit powers on; it's to flag any product that sits too close to the edge of its specification.
A well-structured end-of-line test sequence uses a mix of static and dynamic measurements, often including stress pulses or brief burn-in cycles that expose weak solder joints, marginal capacitors, or drifting references. Test limits are tightened beyond the datasheet values, so a unit that barely passes at ambient temperature but drifts under a slight load gets rejected before it reaches a customer. This catches the “walking wounded”—parts that function in the lab but fail after a few weeks in the field.
The result is a more consistent outgoing quality level and fewer field returns. By investing in smarter end-of-line screening, manufacturers shift the failure curve away from early-life defects. It’s not about testing every possible scenario, but about targeting the specific failure modes that tend to hide in the gray zone between pass and fail.
FAQ
The split-core design demands precise air gap control and a mechanical hinge that keeps the core halves aligned within microns. Unlike solid-core units, every split-core transformer must compensate for the extra reluctance introduced by the parting line, so factories invest more in core grinding, lapping, and gap-filling materials to keep residual current measurement stable.
Core annealing and winding symmetry have the biggest influence. If the core is annealed unevenly or wound with unequal turn distribution, the residual flux becomes unpredictable and tripping thresholds drift. A factory that controls these two steps tightly will see far less variation in 30 mA and 100 mA sensitivity units.
Use batch-level BH curve tracing and impedance analysis on sample cores before winding. High-permeability materials like nanocrystalline or permalloy can vary between suppliers, so a factory should also run temperature cycle tests from -25°C to 70°C and compare magnetizing current at a fixed voltage to reject lots that shift more than a few percent.
Every unit should pass a residual current trip test with a reference leakage current source, a hipot test at 2.5 kV for one minute, and a core balance test with primary current flowing through all phases. Batch samples should also undergo vibration and thermal shock to expose weak hinge or potting interfaces.
Uneven tension changes the copper wire's position on the core and alters stray capacitance. For a residual current transformer, that capacitance can couple noise into the secondary and create false trip signals. Factories that use closed-loop tensioners and measure winding resistance scatter below one percent tend to have far fewer field returns.
Standardize the split point geometry and use a precision fixture for core alignment before potting. Leakage inductance rises sharply when the two core halves do not meet flush, so a go/no-go gauge checking the air gap under a set clamping force is more effective than relying on visual inspection.
Encapsulation locks the core halves and secondary winding in place, prevents moisture ingress at the split interface, and damps micro-vibrations that can shift calibration over time. A flexible polyurethane or epoxy with low shrinkage and high thermal conductivity is usually a better choice than rigid compounds that can crack the core.
For global acceptance, align with IEC 62020 for residual current monitors, IEC 61869-2 for current transformers, and UL 1053 where North American ground-fault protection applies. Factories that test to these standards in-house, not just at external labs, can catch design drift much earlier.
Conclusion
A dependable split-core residual current transformer starts with honest material selection. Low-loss, high-permeability cores keep magnetizing current predictable so leakage readings don't drift with temperature or frequency. Winding tension is not a trivial setting; inconsistent pull deforms wire insulation and alters leakage inductance just enough to blur the trip threshold. When the two core halves come together, the factory must treat the mating surfaces as a magnetic joint, not a mechanical one. Precision grinding and controlled clamping reduce air-gap reluctance so the split-core design doesn't sacrifice sensitivity for installation convenience.
Protecting that assembly matters as much as building it. Encapsulation compounds need to resist moisture, thermal cycling, and chemical exposure without stressing the core or shifting calibration. Calibration itself should be done under fault-like conditions—unbalanced currents, harmonic-rich waveforms, and temperature extremes—not just sine-wave bench tests. Finally, end-of-line testing has to be strict enough to catch units that pass nominal specs but fail under marginal conditions, because a residual current transformer that only works in ideal settings is a safety liability.
Contact Us
Contact Person: Liu Mengyang
Email: [email protected]
Tel/WhatsApp: 8618727589233
Website: https://www.cnlrm.com/en/