Private Label Film Sandpaper: A Complete Guide to Custom Abrasive Solutions
2026-09-30
If you’ve ever fought with store-bought sandpaper that loads up or tears mid-job, this one’s for you. Private label film sandpaper flips the script: you decide the backing, grit, and branding—not the shelf. In this guide, we break down what custom abrasive solutions actually involve and why SHENZHEN SUN ABRASIVES is worth a close look.
What Actually Sets Film-Backed Abrasives Apart
Unlike paper or cloth backings, film is a solid extruded polyester sheet with no fibrous weave or pulp grain. That means the abrasive particles sit on a surface that's nearly perfectly flat from edge to edge, eliminating the microscopic bumps and valleys that can cause uneven scratch patterns. The result is a more consistent scratch depth across the workpiece, which matters when you're chasing a uniform finish.
Film backing also resists tearing, stretching, and curling under load. Paper can soften or tear when wet, and cloth can flex too much, but film holds its shape even during aggressive sanding or when used with water and lubricants. That dimensional stability lets you apply more pressure without the backing deforming, so the abrasive cuts longer and wears more evenly instead of folding or fraying at the edges.
Another difference is how film-backed abrasives handle heat and debris. The non-porous surface doesn't absorb coolant or dust, so particles don't get trapped beneath the abrasive layer. Less clogging means faster cutting and fewer random deep scratches from stray grit. For fine finishing or high-tolerance work, that predictability is often the deciding factor over conventional backings.
Designing the Backing for Specific Surface Demands
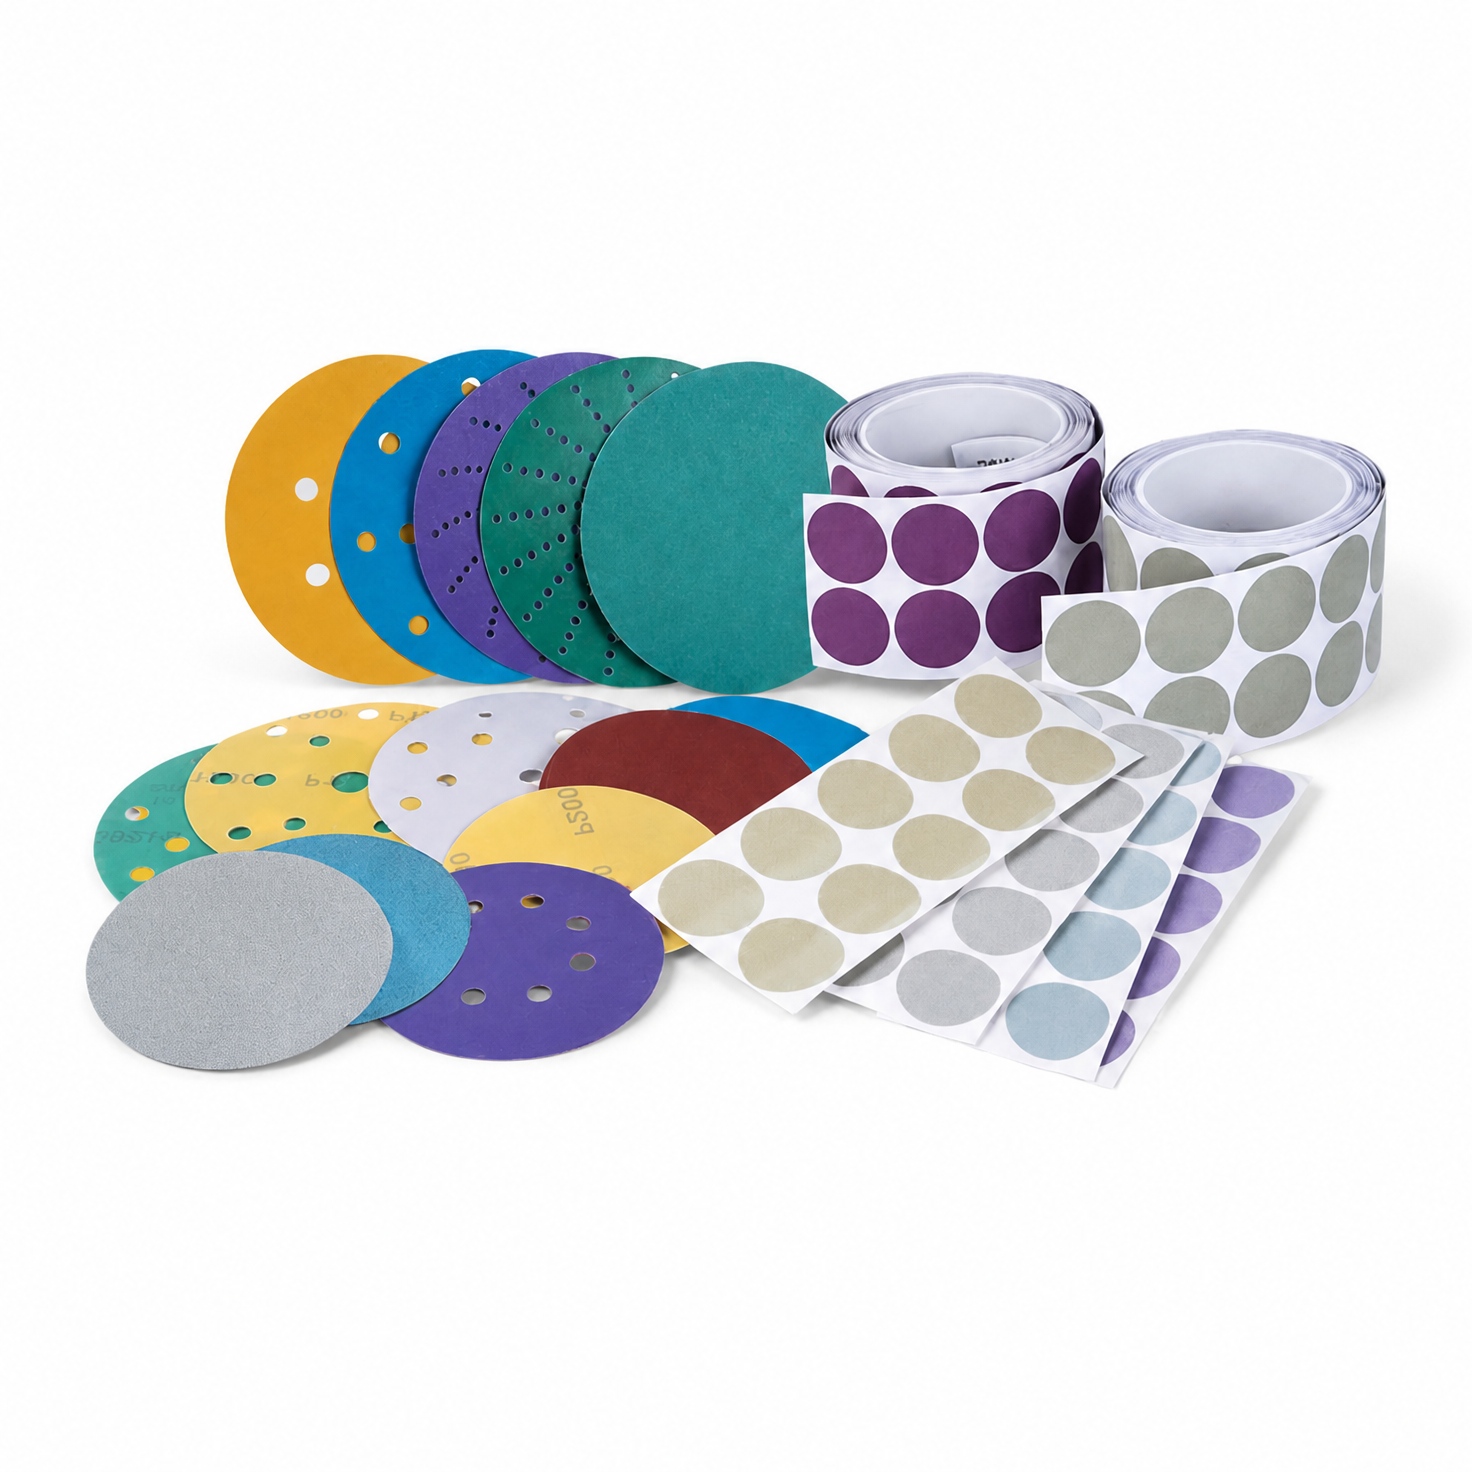
Every substrate brings its own set of rules to the table, and the backing has to be tuned accordingly. A polished concrete floor, for instance, asks for a thin, dense layer with aggressive initial tack, because there's nothing for fibers or foam to bite into. By contrast, a textured wallboard or uneven tile benefits from a more open, compressible construction that can conform to the irregularities without losing contact area. The trick is to balance stiffness and flexibility so the backing neither telegraphs the surface profile nor floats above the low spots.
Moisture and thermal movement further separate one surface requirement from another. In basements or bathrooms, the backing must resist hydrolysis and allow vapor to escape rather than trapping it against the substrate. Where floors expand and contract with temperature swings, a slightly elastic backing prevents edge lifting and keeps the product flat over time. Selecting the right fiber denier, weave density, or foam cell structure, then, is less about generic strength and more about matching the failure mode of the specific surface you're covering.
Grit Selection: Matching Abrasive to Outcome, Not Just Spec
Many shops treat grit numbers as rigid steps, moving from 80 to 120 to 220 without asking what the surface actually needs. The spec sheet tells you particle size, but it doesn't tell you how that abrasive will cut your specific material, leave a particular scratch pattern, or prepare the surface for coating. Outcome-driven selection starts with the end state: are you removing mill scale, leveling a weld, or chasing a mirror polish? Each goal demands a different starting point and often a non-linear progression.
A finer grit doesn't always mean a better finish. On soft metals, high grit can smear rather than cut, embedding particles and creating more cleanup later. On hard coatings, skipping an intermediate step might leave deep scratches that no amount of fine sanding will erase. The real skill is matching abrasive type and grit to the material's hardness, the depth of defects, and the tolerance for subsurface damage. For painted surfaces, you might jump from 180 to 320 and stop; for stainless going to a brushed finish, 120 followed by a non-woven pad can beat a full grit ladder.
Don't ignore the role of pressure, speed, and backing pad. Those variables change how a given grit performs far more than the number on the package. A 220 disc on a stiff backup will cut differently than the same disc on a soft interface. Testing on scrap reveals more than any chart. Let the result—gloss, flatness, adhesion—be the judge of whether the grit matched the outcome.
Beyond Logos: Customization That Changes How It Performs
Customization rarely goes deeper than slapping a logo on a stock product. But what if the way something is tailored actually reshapes its behavior? That's the difference between decoration and genuine adaptation. When design choices affect performance, the object stops being a branded version of the same thing — it becomes a tool tuned to a specific way of working.
Consider how a change in material or weight distribution can shift balance, grip, or response time. These aren't cosmetic tweaks; they alter how the item functions in real hands. The result is a piece that doesn't just look like yours, but acts like yours. It responds differently under pressure because it was built around your patterns, not just your preferences.
This kind of customization demands a more thoughtful approach from both maker and user. It requires mapping actual usage scenarios, not just aesthetic tastes. When done well, the customized object feels less like a purchase and more like a collaboration — one where the final form emerges from a dialogue between need and craft, rather than from a color palette alone.
Quality Checks That Catch What Standard Testing Misses
Most test suites rush through the happy path and call it done. A login form gets checked with a valid username and password, maybe an incorrect one. But nobody pastes a password with a trailing space, types an email address with an emoji in the local part, or double-clicks submit before the first request finishes. Those gaps aren't exotic; they are exactly how real users break things. Quality checks that matter start by listing assumptions the product silently makes and then violating each one on purpose.
A second blind spot is failure behavior. Standard testing confirms what happens when every dependency returns a clean 200. It rarely checks the moment after a third-party API starts rate-limiting, or when a database query takes eight seconds instead of eighty milliseconds. If the interface freezes, shows a blank screen, or retries in a loop, that's a quality failure no unit test will flag. Good checks force slow responses, malformed payloads, and dropped connections, then watch how gracefully the system recovers.
The most useful checks aren't written from a specification; they are extracted from what already went wrong. Support tickets, error logs, and postmortems contain patterns that standard test cases ignore. Turn those incidents into small, repeatable probes. A checkout flow that failed because a customer used an address longer than 60 characters becomes a check. A search bar that crashed on a single emoji becomes another. This keeps the test suite rooted in actual usage, not imagined requirements.
Building a Private Label Program Without the Usual Headaches
Most private label launches stall because operators try to copy a national brand instead of fixing an actual gap on the shelf. Start by picking a handful of high-turn items where the existing options are overpriced or underwhelming, then work backward from the customer complaint you hear most often. That keeps the assortment tight and gives your buying team a clear reason to say yes to a new SKU.
The headaches usually show up later in the supply chain, not in the idea. Instead of chasing a dozen low-volume suppliers to save a few cents, partner with one or two contract manufacturers who already run clean lines and can handle smaller runs without punishing minimums. Write the spec so the product has to match a reference sample, not a vague description, and schedule a production audit before the first purchase order goes out.
Finally, treat the launch as a test, not a commitment. Run a limited store or online pilot, give the item a clear but understated label, and collect sell-through data for six to eight weeks. If the numbers work, scale up; if not, kill it fast and move on. That discipline removes the fear that usually makes private label feel risky.
FAQ
Film backings are polyester-based, so they resist tearing, offer more consistent thickness, and flex without cracking. That translates to a more uniform scratch pattern on contoured surfaces, especially in wet sanding where paper would swell or fall apart.
Automotive refinishing, aerospace composites, woodworking, and metal fabrication are the big ones. Any operation that needs a durable abrasive for fine finishing or precise surface prep tends to move toward film products, particularly when they want their own branding on the package.
Absolutely. You can specify the film thickness, abrasive grit type and size, coating density, backing color, edge profile, and even perforation patterns. Some suppliers also offer custom print on the non-abrasive side so the product carries your logo or usage instructions directly.
Thinner films around 1 mil to 2 mil wrap tightly around small contours and are great for feather edging. Mid-range 3 mil films strike a balance between flexibility and durability. If you are working on sharp edges or need aggressive stock removal, a 5 mil or thicker film will hold up longer without tearing.
Most programs cover everything from coarse 60 or 80 grit for rough sanding up to 3000 grit or finer for color sanding and polishing. The key is matching the grit to your substrate and finish goal, not just picking the finest option available.
It varies by manufacturer, but many private label programs start around 1,000 to 5,000 discs or sheets per SKU. Some suppliers offer lower trial runs if you are testing the market first, though unit costs will be higher at small volumes.
Ask your supplier about their incoming film inspection, coating weight control, and final visual checks. Reputable private label partners will provide lot traceability and may share test results for coating adhesion, grain retention, and backing tensile strength before shipping each run.
Conclusion
Film-backed abrasives earn their keep by doing what paper and cloth can't: the polyester film backing stays uniformly flat and resists tearing even when wet, which translates to a more consistent scratch pattern and longer life on demanding surfaces. But the real advantage shows up when you stop treating the backing as a fixed given. Pets, plastics, automotive clear coats, and wood each respond differently to rigidity, thickness, and flex. Matching the film's stiffness to the substrate prevents edge cutting and gouging while still allowing enough give for contoured areas. Grit choice follows the same logic. Instead of settling for a generic FEPA or ANSI number, you work backward from the final surface quality: a 600-grit film on a soft backing might leave a different finish than the same grit on a rigid one. That's why private label programs benefit from sample testing across actual workpiece materials, not just spec sheets.
Customization goes well beyond printing a logo on the backing. Abrasive grain type, open versus closed coat, anti-loading stearates, and even the adhesive bond can be tuned to change how the product cuts, clears swarf, and resists heat. A shop sanding freshly painted panels needs a different anti-clogging package than a metal fabricator chasing a matte finish. Quality control should mirror these real-world demands: standard grit size and tensile tests miss problems like backing curl under heat or premature loading on tacky surfaces. A good private label partner will run simulated use tests, measure cut rate over time, and check edge wear on typical contours. For the brand owner, that means fewer field failures and less guesswork. Setting up a private label line doesn't have to be a headache if the supplier already has proven film bases and a structured sampling protocol; you choose the performance profile, and they handle the film conversion, coating, and packaging. The result is a product that carries your name and actually performs like it was built for your customers' jobs.
Contact Us
Contact Person: Amanda Wang
Email: [email protected]
Tel/WhatsApp: +86-13602569854
Website: https://www.sunabrasives.com.cn