How to Choose an Optical Comparator: Key Factors for Precision Measurement
2026-09-22
Precision doesn’t leave room for guesswork. If you’re in the market for an optical comparator, you already know that the wrong choice leads to measurement drift, part rejection, and a lot of wasted time. But the right choice? It comes down to a few details most buyers overlook. From stage travel and lens quality to software that doesn’t fight your workflow, each factor shapes how reliably you capture critical dimensions. At JATEN, we’ve seen how a smart comparator decision saves months of rework. This guide cuts through the spec-sheet noise so you can focus on what actually matters for your inspection room.
Pin Down the Smallest Feature Before Comparing Lenses
Most lens comparisons fall apart because they chase broad impressions instead of a single, concrete difference. Before you line up two or three options, ask what tiny visual signature actually matters for your work: the shape of specular highlights at f/2.8, the transition from sharp to blurred along a jawline, or the way a 35mm handles foreground distortion. If you cannot name that one feature, every test chart and sample gallery will blur into noise.
Once that smallest feature is pinned down, comparing lenses becomes a filtering exercise rather than a vague ranking. You might ignore center sharpness entirely if your frames live at the edges, or dismiss chromatic aberration if you shoot black and white. The lens that wins is rarely the one with the highest overall score; it is the one that renders that specific detail the way you already see it in your head.
Don't Ignore Stage Travel Until a Large Part Shows Up
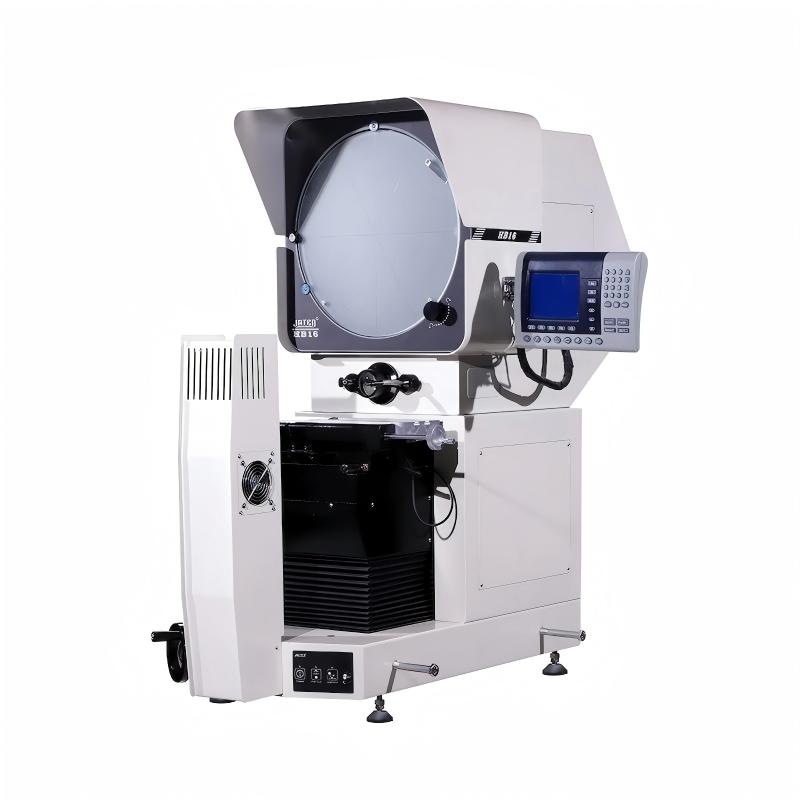
Many actors treat stage travel as a minor chore, something to polish only when a leading role lands in their lap. That mindset backfires. The way you cross from one side of the stage to the other, the pauses you take near a prop table, even the angle of your turn mid-line—these small choices accumulate into presence. If you ignore them until a big part shows up, you'll be learning basic movement under pressure, and the audience will sense the hesitation.
Consider stage travel as muscle memory for your feet. Just as you wouldn't skip vocal warm-ups for months and expect to nail a demanding aria, you can't expect your body to glide naturally across the boards after weeks of standing still. Work on it in every rehearsal, even for a walk-on role with no lines. Use the empty stage to map out your own paths, test different speeds, and find what feels honest. By the time a large part does show up, the travel will feel like second nature, and you can pour all your energy into character instead of worrying about where to put your feet.
Optics Quality Is More Than a Specification Sheet Number
A specification sheet can list impressive numbers for resolution, light transmission, and chromatic aberration, but these figures rarely reflect how an optic performs in the hand. Real-world quality shows up in the way a binocular controls stray light when a bright source sits just outside the field of view, or how a riflescope maintains contrast as the sun drops low. Those behaviors come from baffle design, internal blackening, and careful placement of every lens group—details that never make it onto a data table.
Glass selection and coating quality matter just as much as the final numbers. Two lenses can have identical focal lengths and apertures, yet one delivers a flat, washed-out image while the other reveals subtle color separation and deep shadows. Multicoatings vary widely in their ability to suppress reflections without shifting color balance, and low-dispersion glass only reaches its potential when the mating elements are ground and centered to tight tolerances. Assembly precision, not the listed glass type, often determines whether the image snaps into focus across the entire field.
Then there is the part of optical quality that no instrument can measure directly: how your eyes feel after an hour of use. Slight miscollimation, edge distortion, or a color cast too faint to notice in a quick glance can produce fatigue, headaches, or a sense that the view is somehow artificial. A truly well-made optic disappears in front of your eyes, leaving only the scene. That kind of performance is earned through iterative prototyping and field testing, not by optimizing a spec sheet for a brochure.
Lighting Can Turn a Good Comparator into a Great One
Most comparator setups rely on whatever overhead light came with the machine, and that is exactly where the problems start. A single bright source straight down will wash out shallow steps, hide fine scratches, and make fillets look larger than they are. Move that same light to a low angle or use a narrow slit beam, and details that were invisible seconds earlier suddenly have sharp, measurable boundaries.
The real trick is to treat lighting as an adjustable part of the measurement loop. For turned or ground parts, a soft ring light at roughly 30 degrees off the surface brings out lay marks without creating hot spots. For through-holes and profiles, a collimated backlight gives you a crisp silhouette that makes edge detection almost boringly reliable. If you are inspecting transparent or polished materials, polarized light can cut reflections that would otherwise fool the comparator's edge-finding routine.
Spending ten minutes swapping or repositioning lights is not extra work. It is often the difference between catching a borderline part and shipping a reject. When operators get comfortable changing lighting to match the feature they are checking, the same comparator starts delivering measurements that feel like they came from a more expensive system.
Software That Cuts Setup Time Without Dumbing Down the Process
Most setup-reduction tools force a choice: save time or keep full control. This software refuses that trade-off. It trims repetitive steps—auto-filling proven toolpaths, pulling part geometry and tooling data from previous jobs, and flagging only the parameters that genuinely need a decision—while leaving every advanced setting accessible. Operators can work in a streamlined view for routine work but drop into the full process definition without switching applications or exporting data.
The result is less time spent re-entering the same information and fewer errors from overlooked details. A job that used to take forty minutes of prep now takes fifteen, not because options were hidden, but because the software learned what your shop already knows. It groups related parameters, warns when a value falls outside your typical range, and lets supervisors lock down only the parts that must stay consistent. Skilled machinists don't feel constrained—they can still adjust feeds, speeds, and offsets at any point. The difference is that the software handles the mechanical busywork, so human attention goes where it actually matters.
Real-World Repeatability Starts With How You Anchor the Fixture
Ask anyone who has chased a tolerance drift across shifts and they will eventually point at the fixture. Not the part clamping, not the tool offsets—the way the fixture itself is bolted to the machine table. That joint is where real-world repeatability is born or lost. A fixture that rocks, shifts, or settles under load turns even a rigid machine into a random number generator.
Effective anchoring is less about brute force and more about geometry. Start by mapping the actual contact points between the fixture base and the table. Three well-defined pads beat six unknown high spots every time. Replace standard washers with hardened, ground versions to reduce embedding, and if the fixture overhangs the table edge, add a support leg rather than relying on plate stiffness. The goal is to make the fixture behave as if it were machined from the table itself.
Don't ignore the human factor. Two technicians can anchor the same fixture and get different repeatability, purely because one tightens bolts from the center outward and the other from left to right. Write down the sequence and torque values, then verify with an indicator after the first few cycles. A fixture that moves a tenth of a micron during setup will show up as a full micron at the feature level—and that is usually enough to fail a capability study.
FAQ
Start with the part geometry you need to inspect. Complex profiles with tight tolerances demand a larger screen and higher magnification range, while simpler turned parts can often be handled by a compact benchtop unit. Matching the machine to the actual workpiece—not the theoretical maximum—usually saves both floor space and budget.
It depends on the smallest feature you have to measure or verify. Many shops find 10x and 20x lenses cover most routine checks, but if you're working with fine threads or micro-features, a 50x or even 100x option makes sense. Just remember that higher magnification shrinks the field of view, so you'll spend more time repositioning the part.
For repeat measurements and data logging, yes. A digital readout removes the guesswork from interpreting scale positions and reduces operator error. That said, if you only need occasional go/no-go comparisons against an overlay chart, a purely optical unit can still be perfectly serviceable.
More than people expect. A slotted table with decent travel and a solid locking mechanism lets you handle heavier or awkwardly shaped parts without building custom fixtures. If your work involves long shafts or tall components, check both the vertical capacity and the throat clearance before committing.
Profile lighting is ideal for crisp edge detection on silhouettes, but surface lighting is what reveals recessed details, blind holes, or engraved marks. Many precision tasks benefit from having both, especially when you need to inspect features that don't show up clearly in a transmitted light path.
Vertical machines work well for flat parts and are often easier to load, while horizontal designs handle turned or cylindrical workpieces more naturally. If most of your parts can lie flat on the stage, vertical might be the simpler choice; if you're checking shafts or threaded components, horizontal orientation usually saves setup time.
Screen size mainly affects viewing comfort and the ability to compare a large profile at once. A 14-inch screen is common and adequate for many jobs, but a 30-inch screen helps when multiple operators need to view the image simultaneously or when you're tracing a complex contour by hand.
Modern comparators often integrate with measurement software that can handle geometric dimensioning, export reports, and store part programs. If you're working in a high-mix environment, software with easy overlay creation and automatic edge detection can cut inspection time noticeably, even if the initial setup takes a little longer.
Conclusion
Choosing an optical comparator rarely comes down to a single spec. Start with the smallest feature you actually need to resolve—lens selection follows from that, not the other way around. Stage travel gets overlooked until a large part arrives and suddenly the area you need to inspect sits beyond the reach of the table. Check the X-Y travel against your largest expected workpiece, including any fixture that might overhang. Optics quality is more than a number on a data sheet; edge-to-edge clarity and distortion matter when you're measuring a thread flank or a radius at the outer edge of the field. And lighting deserves as much attention as the lens. A well-placed profile light or oblique surface illuminator can reveal a burr or a worn edge that a higher magnification lens would only blur.
Software should cut setup time without hiding the actual measurement logic. Look for quick alignment tools and saved part programs, but make sure you can still verify what the system is measuring rather than trusting a black box. Finally, real-world repeatability starts with how you anchor the fixture. If a part can shift even a few microns between loading cycles, no optical quality or software correction will recover that lost precision. Use positive stops, vee blocks, or dedicated nests that locate the datum features the same way every time. A comparator becomes a reliable gage only when the lens, stage, lighting, software, and workholding all support the same measurement task.
Contact Us
Contact Person: Volien
Email: [email protected]
Tel/WhatsApp: +86 18029161762
Website: https://www.jatentech.com/