DC Combiner Box Factory: Expert Manufacturing for Solar Energy Systems
2026-09-04
Most solar failures don't start in the inverter—they start in the box that quietly collects every string of DC power before it ever reaches conversion. That's why a DC combiner box is more than a junction: it's a critical safety and performance layer. At Chang Song's factory, those boxes are built by a team that treats DC-side protection as a specialty, not an afterthought. From pre-wired busbars to outdoor-rated enclosures, the details are visible long before the first module is plugged in. Here's what expert manufacturing actually means for your next solar project—and why the factory behind the box can be the difference between a smooth commissioning and a recurring service call.
Where Busbars Meet Brawn: Our DC Combiner Assembly Floor
The floor hums with a low, metallic rhythm—copper busbars being positioned, torqued, and double-checked under work lights that rarely dim. Here, brawn isn't a buzzword. It's the controlled force behind every lug crimp, the way a technician leans into a wrench to hit the exact spec, and the shared glance between two crew members before a heavy enclosure swings into place.
Our DC combiner line runs on more than procedure. You'll see hand-sketched torque maps taped to station frames, a breaker cart with its own battle scars, and a test bay that has rejected more connections than most floors assemble in a week. That friction is intentional. If a busbar doesn't seat square or a bolt stretches past tolerance, the whole line stops until the cause is found—not just the symptom patched.
What gets built here survives because the people on this floor treat every combiner as if it's going into their own array, in a location they'll never visit. That's the standard that keeps our busbars straight, our labels honest, and our brawn aimed at one thing: connections that hold when the sun does the rest.
Custom Enclosures That Match Your Array, Not the Other Way Around
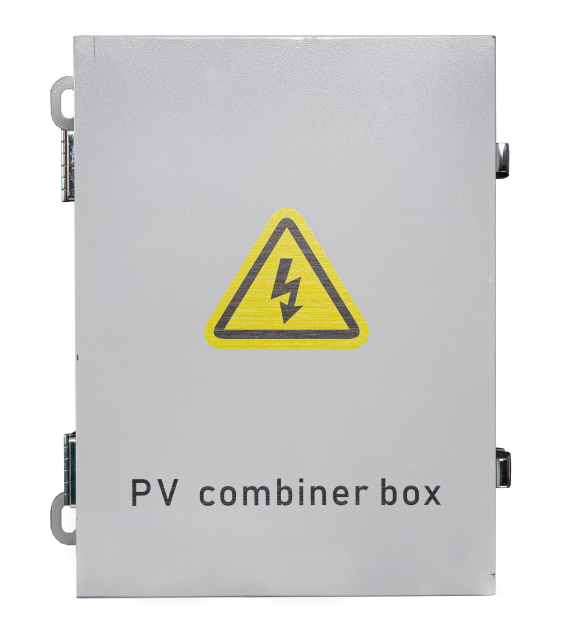
Most enclosure makers start with a box and expect your array to squeeze inside. We don’t. We measure the actual layout, driver spacing, depth, and port requirements from your system first, then build the enclosure around those numbers. The result is a cabinet that feels like part of the original design, not an afterthought.
That means no more shimming brackets, no more cutting into baffles, and no more praying the rear chamber volume works out close enough. Our process accounts for the slight variances between individual boxes in an array, so each enclosure lands exactly where it should without forcing the rig into a generic footprint.
When the enclosure matches the array instead of the reverse, setup gets faster and the whole stack sits tighter. You keep the tuning, the coverage, and the look you already rely on—we just give it a proper home.
The Quiet Engineering Behind Fewer Arc Faults
Most arc-fault reduction never appears on a specification sheet. It sits in the choice of contact geometry, the slight taper on a bus bar, or the way a connector's spring force is tuned so thermal cycling doesn't loosen the mating surfaces over time. These adjustments rarely get named in failure reports, but they consistently shift wear patterns away from intermittent arcing.
Insulation coordination follows the same quiet logic. Engineers expand creepage paths not by rewriting standards but by reshaping a housing rib or moving a seam just far enough outside the high-field region. Tightening tolerance control on ferrule crimps and softening sharp edges near energized parts further lowers the chance that a partial discharge turns into a sustained arc.
Weatherproofing Beyond the IP Rating Plate
Most people treat the IP rating plate as the final word on weatherproofing, but that little two-digit code only tells you how a product performed under a very specific set of lab conditions. Real weather doesn't read spec sheets. It cycles from dry heat to freezing rain, pushes water uphill through capillary action, and attacks the housing materials themselves long before liquid ever reaches the seals. So instead of stopping at IP66 or IP67, look at how the enclosure handles thermal expansion, condensation, UV exposure, and repeated pressure washing.
A common overlooked failure point is the gasket. Even a premium silicone or EPDM seal will eventually take a set if the lid is over-torqued or if the housing flexes during temperature swings. That means the IP rating becomes meaningless when the gasket loses its rebound. Check whether the design includes a controlled compression stop, and whether the material is rated for both high heat and sub-zero stiffness. The same goes for cable glands and conduit entries: they need to be specified for the actual cable diameter and outdoor exposure, not just chosen from a generic compatibility chart.
Drainage and breathing also matter more than many designers admit. A fully sealed box can trap moist air inside, causing condensation that destroys electronics from the inside while the outside stays perfectly dry. Adding a breather vent or a factory-installed drain hole often does more for long-term reliability than chasing a higher IP number. So when you're evaluating weatherproofing, look past the plate. Ask how the enclosure behaves after five years of sun, salt, and temperature shock—not just how it scored on a 30-minute spray test.
A Factory Test Regime That Earns Its Keep in the Field
Most factory test regimes are little more than a final gate: power on, run a few canned routines, ship it. That misses the point. A test line that truly earns its keep in the field is built around stress margins and parametric drift, not binary pass/fail. For instance, instead of merely verifying that a voltage rail sits within tolerance at room temperature, you measure how much that rail sags during a rapid load step, then track the same unit across thermal cycling. The resulting data tells you whether the product will still meet spec after six months of real-world abuse, not just on day one.
The sequencing matters as much as the individual checks. A regime that pays off later mirrors actual usage patterns in compressed form: repeated power cycles with abrupt brownouts, vibration profiles lifted from field recordings, and sustained operation at the edge of the thermal envelope. No single test is exotic; it's the combination and order that exposes weak solder joints, marginal capacitors, or firmware race conditions that only appear after a cold start. When a failure occurs, the line doesn't just flag the unit—it logs the exact step, the environmental conditions, and the parametric readings leading up to it. That log becomes the starting point for root cause analysis, not a mystery to be recreated weeks later.
The real payoff shows up in warranty data and service calls. Products that pass a well-designed factory regime tend to fail less often in the first year, and when they do fail, the failure mode is usually one you've already seen and can fix quickly. This isn't about adding more tests for the sake of coverage metrics; it's about choosing the few tests that correlate with field reliability and letting them evolve as field returns teach you what you missed. A test line that never changes is just burning cycle time.
Scaling From Single-String Jobs to Utility-Scale Solar Farms
What starts as a weekend crew pulling a few hundred feet of wire through a residential inverter quickly turns into a different beast when the same company lands a 200-megawatt ground-mount. The jump from single-string jobs to utility-scale solar farms isn't just about adding more panels—it rewires how you plan, procure, and manage crews across miles of racking.
On small jobs, a missed connector or a slightly off torque spec might cost an hour. On a utility-scale site, that same oversight repeats across thousands of piles and can stall an entire substation handoff. Successful teams stop thinking in terms of individual strings and start treating the site as a series of repeatable, modular blocks—each with its own QC gate, material staging area, and clear handoff between civil, mechanical, and electrical crews.
The shift also demands a different relationship with data. String-level monitoring gives way to inverter-level and SCADA-level diagnostics, while daily production targets are tracked against planned MW rather than kilowatt-hours per roof. Companies that thrive at utility scale typically build out a dedicated pre-construction team, standardize torque and tension logs, and accept that the real bottleneck is rarely installation speed—it's keeping trenching, pile driving, and module placement from drifting out of sequence.
FAQ
We run a dedicated sheet metal and busbar workshop in-house, so every enclosure and copper path is checked before wiring begins. This cuts out the usual back-and-forth between subcontractors and lets us hold tighter dimensional tolerances on high-current connections.
Each unit passes a hipot test at twice the rated voltage plus 1000V, followed by insulation resistance checks and a thermal scan under full load. Only boxes that stay within a 10-degree rise window leave the floor.
Yes, we regularly build from 4-string residential boxes up to 32-string units with 20A or 25A fuse holders, touch-safe barriers, and optional surge protection. Customer drawings are reviewed within 48 hours and a pre-production sample is shipped for approval.
Standard cabinets are powder-coated steel rated IP65, but we also supply stainless steel and fiberglass versions for coastal or high-UV sites. Before assembly, every gasket groove is inspected for flatness to prevent dust ingress and condensation.
Each shipment includes a serialized test report, one-line diagram, torque values for terminals, and QR-linked wiring labels. We also keep a digital copy of the build record for at least ten years.
We work directly with three breaker manufacturers and stock both 1000V and 1500V DC-rated models. Instead of relying on spot purchases, we keep a rolling six-week inventory for common ratings and only use UL-listed fuse holders inside the box.
A typical order of 200 to 500 boxes leaves our facility in four to five weeks after drawing approval. We can compress that to three weeks for repeat builds with no design changes, and we stagger shipments to match site progress.
Conclusion
Walking the assembly floor where busbars are cut, punched, and torqued gives a clearer picture of why a DC combiner box holds up over time. The enclosures are not pulled from a generic catalog; each one is sized around the actual string count, fuse type, and cable entry points of the array it will serve. That approach removes crowded terminations and makes field wiring less error-prone, and it cuts down on the kind of loose connections that show up later. On the electrical side, the quiet work happens in how busbar routing, creepage distances, and terminal placement are arranged to keep potential arc faults low before they ever reach a protection device.
Weather sealing here goes past a printed IP code. Gaskets are compression-tested, drain holes are positioned for real condensation, and powder coat adhesion gets checked after thermal cycling. Every box leaves the floor only after a test sequence that includes insulation resistance, continuity, and trip verification under load. Because the same assembly steps and test fixtures are used whether the order is for a single-string residential job or several hundred combiners for a utility-scale plant, the consistency carries into the field. It is a factory setup built around repeatability rather than rush orders.
Contact Us
Contact Person: Tonglun Chen
Email: [email protected]
Tel/WhatsApp: 8618906642555
Website: https://www.cncsele.com