Collapsible Silicone Kettle Original Manufacturer: Key Benefits and Buying Insights
2026-11-18
A collapsible silicone kettle sounds like a clever travel idea, but the real difference starts long before it reaches your bag. In this guide, we look at what separates a dependable original manufacturer from countless low-cost imitations, and why Qunhao has become a name worth knowing if you are sourcing for outdoor brands, camping gear lines, or everyday carry collections.
What Daily Use Reveals That Product Photos Never Show
Studio shots make every surface look untouchable, but after a week of actual use you notice the little things no lens ever captures. The way a matte finish goes slightly slick near the buttons, how a supposedly compact design still catches on your pocket seam, or where dust settles into the gap between two panels. These are not flaws you can see in a gallery; they show up as routine, almost invisible friction that shapes whether you reach for the item or leave it behind.
Daily handling also reveals sound and texture that photos cannot convey. A latch that clicks with a dull plastic thud instead of a crisp snap, a strap that softens unevenly after repeated wear, or a surface that feels colder than expected first thing in the morning. None of this appears in a hero image, yet it quietly defines the experience more than the polished curves ever will.
Then there is the question of upkeep. Product pages rarely show how a pale interior picks up dye from a jacket, how a glossy front smudges within minutes, or how much effort it takes to keep a design looking the way it did on day one. Living with something long enough teaches you which details were considered and which were styled only for the photograph.
The Difference Between a Trading Company and the Factory That Actually Molds the Silicone
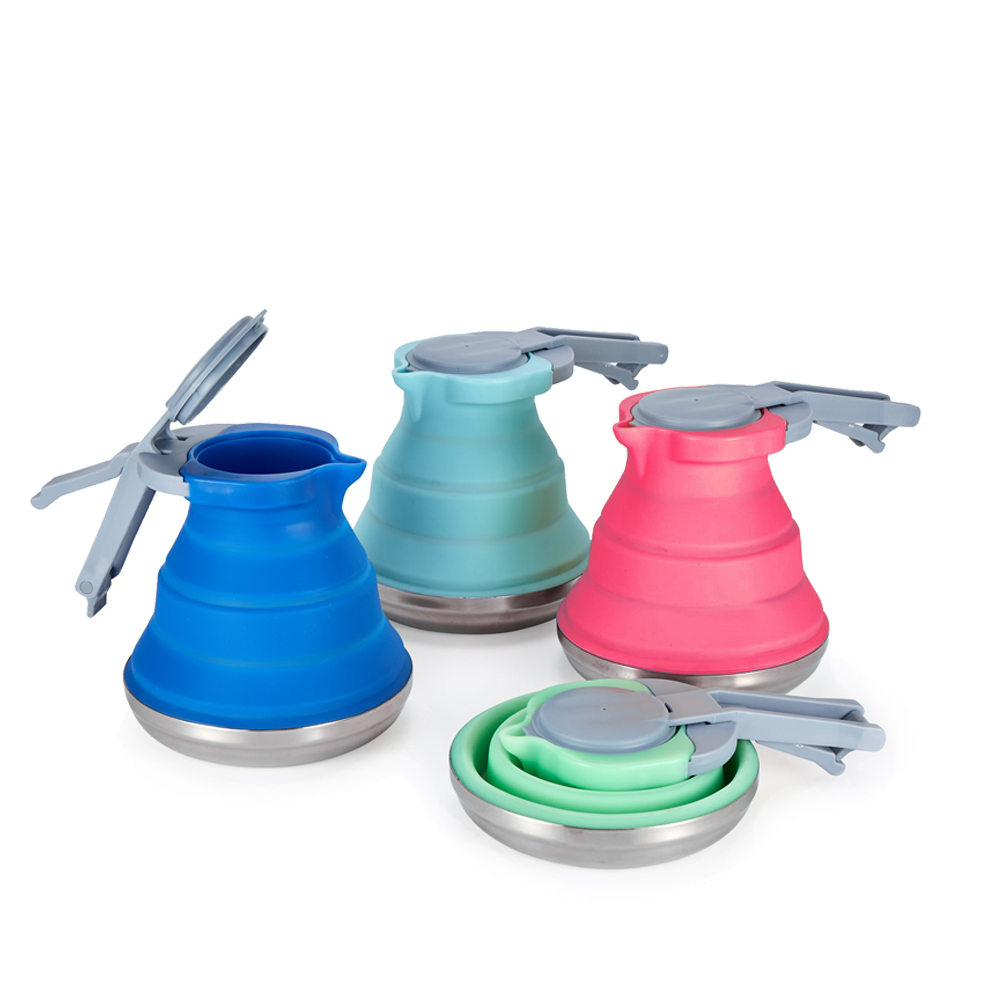
A trading company and a factory that actually molds silicone parts are not separated by a small operational gap; they sit on opposite sides of the process. A trading company usually handles orders, documents, and supplier communication, but it does not own the mold shop or run the press. When a drawing gets sent over, the person answering the email is often not the person who will set the mold temperature or check the flash line.
That distance shows up quickly in technical discussions. A real molding factory can talk about gate placement, parting line mismatch, venting, and tear strength because those details come from the shop floor. A trading company typically has to relay the same question to a subcontractor and return an answer later. If something shifts in the schedule or the material lot changes, the trading company may not know until the shipment is already delayed.
Responsibility also lands differently. A factory that cuts the tool and runs the silicone has to live with the mold, so it tends to flag undercuts, thin walls, or difficult demolding angles before sampling. A trading company may promise a solution and only discover the problem after the sample comes back from an outside workshop. For custom silicone parts, the practical difference usually comes down to whether the person you are talking to can make a change on the floor or has to ask someone else to do it.
Why the Same Foldable Kettle Can Feel Completely Different Across Suppliers
Two foldable kettles can look nearly identical in a side-by-side photo, yet one feels reassuringly solid while the other flexes under light pressure. Much of that comes down to the silicone compound itself. A higher-grade food-safe silicone holds its shape after repeated folding and returns to a tight, smooth form, whereas cheaper blends may thin out at the crease lines, develop a cloudy film, or carry a faint chemical smell after the first boil. Wall thickness and the placement of internal support rings also shift the tactile experience: some kettles stand firm on a table, while others have a subtle wobble that never quite goes away.
The heating base is another place where suppliers quietly cut corners. A sturdy base with a well-seated heating plate transfers heat evenly and brings water to a rolling boil without a metallic aftertaste. In lower-cost versions, the controller may cycle too aggressively, leaving hot spots near the element or producing a plastic-tinged odor from the housing. The cord and plug add to the impression as well—one kettle might have a thick, flexible lead that stays cool, while another arrives with a thin cord that stiffens when warm and makes the whole unit feel temporary.
Small assembly choices ultimately separate a kettle that feels precise from one that feels loose. The lid latch, the way the handle locks in the upright position, and the smoothness of the fold-down motion all reflect how tightly the factory controls tolerances. Some suppliers align the steam vent and lid seal so the kettle opens cleanly without dripping, while others leave rough edges or a slight misalignment that users notice every time they pack it away. These details rarely show up on a spec sheet, but they define whether the product feels like a carefully made tool or just another copy.
When Lower Unit Prices Start Eating Into Your Long-Term Margin
There's a quiet temptation in watching the per-unit cost drift downward. On paper, the spreadsheet lights up: better terms from a bigger supplier, a cheaper material swap, a packaging tweak that shaves pennies. What gets overlooked is how those same pennies quietly dismantle the margin you were counting on three years from now. Lower unit prices almost always arrive with trade-offs that don't show up on the purchase order. Maybe the new vendor ships slower, forcing you to hold more safety stock. Maybe the cheaper resin means more rejects on the line, or more warranty claims six months after delivery. The cost didn't disappear; it moved somewhere harder to see.
The real damage tends to surface when volume grows. You secure that nice low unit price, celebrate the win, then watch as the hidden expenses scale right alongside your sales. Every extra unit now carries a little more rework time, a little more inbound inspection, a little more customer service follow-up. Your gross margin percentage looks stable from a distance, but the actual dollars left after all the friction tell a different story. Teams often chase the unit price because it's easy to measure and easy to defend in a meeting. The harder conversation is about total cost per good unit delivered to a happy customer.
A better habit is to treat any unit price reduction as a hypothesis, not a victory. Ask what changed to make that number possible. Was it a genuine efficiency gain, or did someone upstream push the burden onto your operation? Sometimes the lower price is real and worth taking. More often, it's a signal that your margin is being borrowed from the future, and the repayment terms are about to get uncomfortable. Watching the full cost curve, not just the invoice line, is what keeps a short-term discount from becoming a long-term leak.
A Closer Look at Seams, Vents, and the Parts Buyers Rarely Inspect
Most buyers run their hands over the obvious panels and call it good, but the real story is usually tucked into the seams. A seam that pulls tight at the corner of a cushion, puckers along a zipper line, or disappears under a coat of paint can hide a rushed repair, poor panel alignment, or material that was forced into place. On clothing and soft gear, lifted threads and uneven stitch spacing are not just cosmetic; they often signal that the material was stretched during assembly and will fail early under regular use.
Vents get even less attention because they sit low, behind flaps, or under trim. Yet a blocked or badly fitted vent is a quick way to trap heat, moisture, or fumes where they should not be. Check that vent openings are actually clear, that mesh or louvers sit flat, and that any rubber or plastic surround has not gone stiff or cracked. If the vent is painted shut, warped, or flaking at the edges, expect problems that will not show up until the first hard rain or hot afternoon.
The small parts are where cost-cutting tends to hide: zipper pulls, drain grommets, clips, weatherstrip ends, and the fasteners inside wheel arches or door jambs. These rarely get replaced until after they break, so seeing one that is new, mismatched, or missing is often a sign of earlier damage or a hasty fix. A buyer who spends five quiet minutes on these spots can walk away from a purchase that photographs well but will nickel-and-dime them later.
Sampling Advice for Teams That Cannot Visit the Production Floor
When you cannot stand beside the line, the next best option is to make the sampling process as visual and repeatable as possible. Send the factory a short video or photo guide showing exactly where to pull units from, how many to take, and what angles to capture. Number the cartons or pallets in advance during a live call, then ask the contact on site to hold each selected unit in front of the camera before opening it. This reduces the chance that someone selects only the best-looking pieces and gives you a more honest read on the batch.
A single point of contact inside the facility makes a real difference. Brief that person on the purpose of the sample, not just the procedure, so they understand why random selection matters. During the call, have them inspect one unit at a time and describe what they feel, smell, or hear if relevant. For visible defects, ask for close-up shots with a ruler or coin placed next to the flaw, and request a second photo from a wider angle so you can judge the scale and location on the product. If the sample needs lab testing, agree on the courier, packing method, and sealing of the sample bag while the camera is still rolling.
Document the session as you go. A shared sheet with columns for carton number, unit number, photo file name, and pass or fail notes keeps the review from turning into a blur of screenshots. After the call, send a brief recap of which units were pulled and what remains open. This gives the factory a clear record and gives your team something concrete to revisit if a later shipment shows the same problem.
FAQ
Ask for full material disclosures, not just a generic 'food-grade silicone' claim. Request batch test reports for LFGB or FDA compliance, check the curing process, and confirm whether the factory mixes its own silicone compound or buys it from an outside supplier. Also look at the stainless steel rim and handle fittings, since failures often happen where silicone meets metal rather than in the kettle body itself.
It removes several layers of margin and gives you direct leverage over tolerance checks, material choices, and rework. Instead of relying on a trading company's photos, you can ask for live video of the molding floor, inspect the heating plate assembly, and set acceptable defect rates before production begins. Factories with their own tooling also tend to be more honest about what can and cannot be changed without new molds.
Look for a reinforced folding crease pattern, a rigid steel or hard-anodized aluminum base, a lid that locks or vents safely, and a handle that does not transfer heat from the spout area. Silicone walls should feel evenly thick, without thin patches at the fold lines. The electrical contacts in the base need to be sealed well enough to survive repeated collapsing, not just bench testing.
Many factories quote a low MOQ for stock designs, often around 500 to 1,000 pieces, but that number can climb quickly if you want a custom color, logo, packaging, or a modified spout. Ask whether the MOQ applies per model or per shipment, and confirm if the factory holds existing mold inventory. If you are testing a new market, negotiate a split order across two or three colors instead of paying for a separate production run.
A compact folded kettle still needs internal support around the base and lid. EVA foam inserts, molded pulp trays, or die-cut cardboard cradles work better than loose bubble wrap. If you plan to sell through e-commerce, ask for a drop-test report and use a box size that keeps the silicone body slightly compressed rather than fully stretched, which reduces tear risk at the creases.
Most established factories can provide LFGB, FDA, or EU food-contact declarations, but they may not proactively prepare them unless you ask. Clarify which market you are entering, whether you need RoHS or REACH documentation for electronic components, and if the test reports match the exact color and material version you are buying. A report for a different colorant or a previous batch is common and should be rejected.
Vague answers about silicone hardness, no in-house testing equipment, samples that look hand-finished rather than production-run, and an eagerness to switch materials to lower the price. If the factory cannot explain its cure time, mold temperature, or tear strength, it is likely relying on guesswork. Pay attention to how they document changes; a good supplier sends a revised specification sheet before changing even a minor component.
Conclusion
A collapsible silicone kettle looks straightforward in a listing, but daily use surfaces problems that studio photos never capture, such as a lid that loosens after ten boils, a handle that stays cool in the demo but turns awkward when the pot is full, or a fold line that begins to whiten and weaken within weeks. This is where the gap between a trading company and the factory that actually molds the silicone becomes impossible to ignore. The original manufacturer controls the raw silicone grade, the mold temperature, the wall thickness, and the curing time, so the same foldable design can feel firm and resilient from one source yet floppy or tacky from another, even when the catalog images look identical.
Chasing the lowest unit price rarely helps once those hidden differences reach your customers. A supplier can shave cost by reducing wall thickness near the base, using a cheaper vent insert, or rushing the seam bonding, and each shortcut eventually shows up as returns, odor complaints, or a lid that no longer seals. Buyers who cannot walk the production floor should still ask for cut samples across the base, sidewall, and spout area, not just a finished sample. Request a short video of the molding and leak-testing process, repeat a boil-and-fold cycle at least five times on the sample, and check the vent and seam with a strong light. Those few steps reveal more about long-term margin and product reliability than a spec sheet or a polished photo ever will.
Contact Us
Contact Person: Cecilia
Email: [email protected]
Tel/WhatsApp: 8619057488653
Website: https://silwatbottle.com